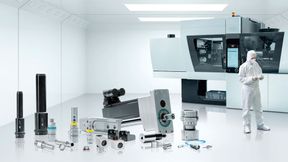
Combining hard turning with internal and external grinding in a single setup can shorten machining times and eliminate reclamping errors. Emag’s VL 100 GT applies this approach to hardened components up to 100 mm in diameter, with integrated loading and in-process measurement.
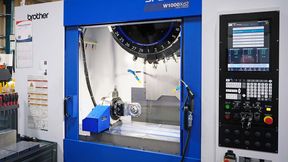
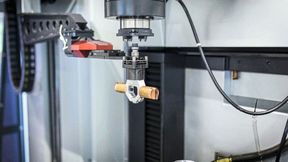
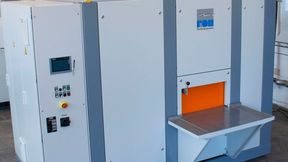
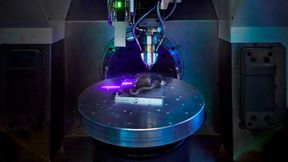
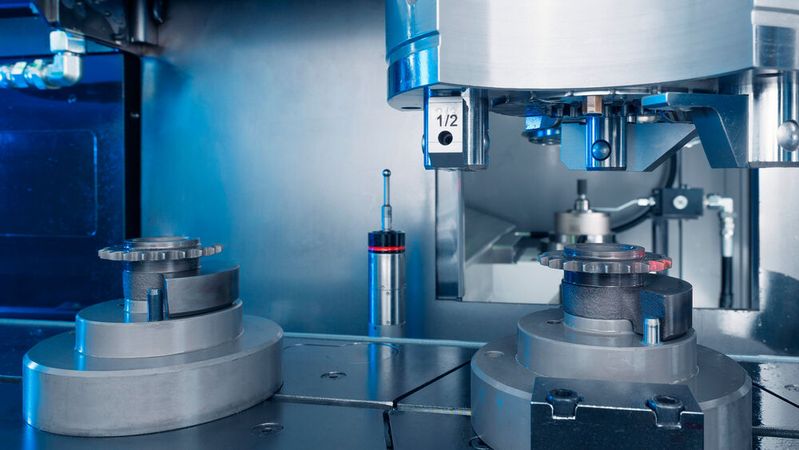
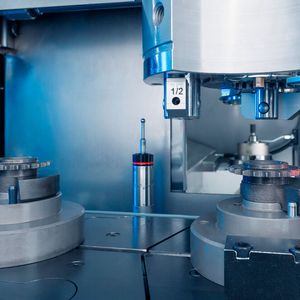
Parts are transported via an O-Automation system. Loading and unloading of the VL 100 GT is based on the pick-up principle. Also shown in the image: the measuring probe.
(Source: Emag)
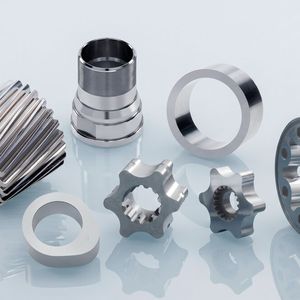
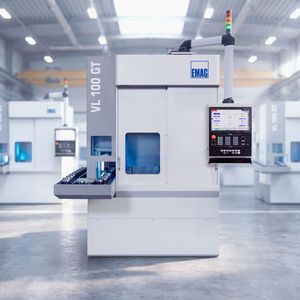
Gear wheels, planetary gears, sprockets, pump rings, individual cams, and wave generators: These chucked components are produced in the millions for medium- and large-volume production. After hardening, each workpiece undergoes precision machining, where dimensional accuracy, surface finish, and positional tolerances must simultaneously be maintained. With the VL 100 GT, Emag offers a vertical turning and grinding center that combines hard turning, internal grinding, and external grinding for workpieces with a diameter of up to 100 mm in a single setup — with a footprint of approximately 9.6 square meters.
Vertical design and Mineralit machine base
The VL 100 GT operates with the vertical machining principle: The workpiece spindle is positioned above the work area and picks up the workpieces from the integrated conveyor belt using a pick-up process. Chips and grinding slurry fall freely downward by gravity without accumulating on the workpiece or the guideways. This reduces thermal interference, prevents surface damage, and minimizes cleaning requirements. User-friendliness is also a top priority with the VL 100 GT: The ergonomically designed work area enables short setup times, and the compact footprint allows for the operation of multiple machines.
The machine base is made of Mineralit polymer concrete, offering eight times greater vibration damping than conventional cast iron. In fine machining, where surface roughness values in the range of Rz < 1.2 µm are required, this damping is a critical factor in achieving quality. The resulting surfaces are free of distortion and meet the requirements for highly stressed functional surfaces in gearboxes.
Integrated pick-up automation
The main spindle handles loading and unloading on its own: It moves to the pick-up station, picks up a raw-part from the circulating conveyor belt of the O-Automation system, moves it into the work area, returns the finished part after machining, and immediately picks up the next raw-part. Separate loading robots or gantry loaders are no longer needed, nor are the associated capital investments. The short travel distances ensure very short chip-to-chip times.
Alternatively, the VL 100 GT can be equipped with shuttle automation for link-up of production lines. In combination with Emag lathes from the VL or VT series, it is suitable, for example, for manufacturing systems ranging from soft turning to hard finishing.
Freely configurable work area
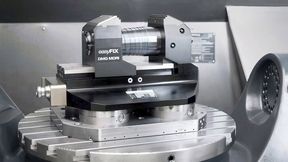
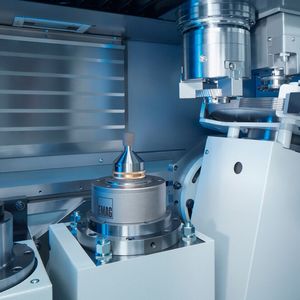
The work area is tailored to the specific workpiece range in consultation with the customer. Available options include internal grinding spindles for bores (corundum or CBN), external grinding spindles for cylindrical surfaces, flat shoulders, and contours, as well as one or two solid steel holders for hard turning operations. This results in configurations ranging from pure internal grinding to a combination of turning and grinding, all the way to complete-machining with turning, internal grinding, and external grinding in a single setup.
A linear motor drive on the X-axis enables the out-of-round grinding of cam profiles and eccentric surfaces. Since the direct drive has no reverse play by design, form errors are avoided during the constant direction changes of the axis. This is a decisive advantage over ball screw drives. Added to this are higher acceleration values and no-wear operation.
Combined machining: cost-effectiveness and quality
The combination of hard turning and grinding in a single setup is a key advantage of the VL 100 GT. In the first step, end faces, chamfers, and flutes are produced by hard turning. These operations are completed much faster by turning than by grinding. Subsequently, the high-precision geometric features — such as bores, O/D (Outer Diameter), and running surfaces — are finished by grinding in the same setup. The hard pre-turning leaves only a few micrometers of stock for the grinding process. This approach significantly shortens the total machining time and eliminates reclamping errors, ensuring the positional relationships between machined surfaces with the highest accuracy. The low material removal during grinding reduces wheel wear, extends dressing intervals, and lowers tooling costs. At the same time, the volume of grinding slurry decreases, which minimizes disposal costs and simplifies the treatment of cooling lubricants. Dry machining is possible in certain configurations.
Date: 08.12.2025
Naturally, we always handle your personal data responsibly. Any personal data we receive from you is processed in accordance with applicable data protection legislation. For detailed information please see our privacy policy.
Consent to the use of data for promotional purposes
I hereby consent to Vogel Communications Group GmbH & Co. KG, Max-Planck-Str. 7-9, 97082 Würzburg including any affiliated companies according to §§ 15 et seq. AktG (hereafter: Vogel Communications Group) using my e-mail address to send editorial newsletters. A list of all affiliated companies can be found here
Newsletter content may include all products and services of any companies mentioned above, including for example specialist journals and books, events and fairs as well as event-related products and services, print and digital media offers and services such as additional (editorial) newsletters, raffles, lead campaigns, market research both online and offline, specialist webportals and e-learning offers. In case my personal telephone number has also been collected, it may be used for offers of aforementioned products, for services of the companies mentioned above, and market research purposes.
Additionally, my consent also includes the processing of my email address and telephone number for data matching for marketing purposes with select advertising partners such as LinkedIn, Google, and Meta. For this, Vogel Communications Group may transmit said data in hashed form to the advertising partners who then use said data to determine whether I am also a member of the mentioned advertising partner portals. Vogel Communications Group uses this feature for the purposes of re-targeting (up-selling, cross-selling, and customer loyalty), generating so-called look-alike audiences for acquisition of new customers, and as basis for exclusion for on-going advertising campaigns. Further information can be found in section “data matching for marketing purposes”.
In case I access protected data on Internet portals of Vogel Communications Group including any affiliated companies according to §§ 15 et seq. AktG, I need to provide further data in order to register for the access to such content. In return for this free access to editorial content, my data may be used in accordance with this consent for the purposes stated here. This does not apply to data matching for marketing purposes.
Right of revocation
I understand that I can revoke my consent at will. My revocation does not change the lawfulness of data processing that was conducted based on my consent leading up to my revocation. One option to declare my revocation is to use the contact form found at https://contact.vogel.de. In case I no longer wish to receive certain newsletters, I have subscribed to, I can also click on the unsubscribe link included at the end of a newsletter. Further information regarding my right of revocation and the implementation of it as well as the consequences of my revocation can be found in the data protection declaration, section editorial newsletter.
Grinding sensors, process control, and measurement technology
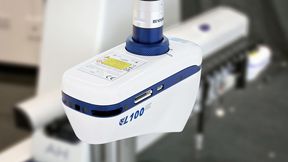
A structure-borne sound system enables contact detection between the grinding wheel and the workpiece, as well as between the dressing roller and the grinding wheel. Adaptive process control monitors the grinding process in real time and adjusts the feed rate to the current machining conditions. Touch dressing is possible. The measuring probe, positioned between the work area and the pick-up station, is protected from contamination. Since the workpiece remains in the setup, measurements can be taken before, after, and between individual machining steps.
Practical example: Sprocket in 35 seconds
A specific application demonstrates the machine’s capabilities: After automatic loading, the bore is finished with a CBN grinding wheel. Subsequently, two block-type tool holders perform machining of the end faces via hard turning. Finally, the integrated measuring probe checks the quality. The entire process takes less than 35 seconds, of which about 10 seconds are spent on workpiece changeover, 15 seconds on hard turning, and 10 seconds on grinding.