A £70 million expansion is increasing manufacturing capacity at Renishaw’s Miskin site in South Wales. The first completed phase brings additional space for metrology and additive manufacturing systems, while energy-efficient buildings and investment in skills support the site’s longer-term development.
Renishaw’s Miskin expansion combines additional manufacturing capacity with investment in employee facilities, apprenticeships and engineering skills.
(Source: Renishaw)
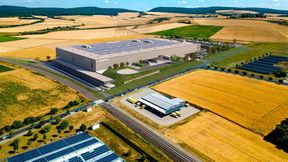
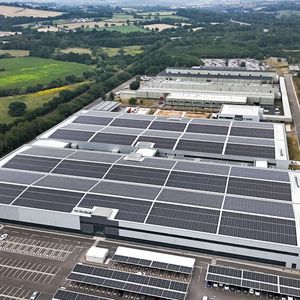
Renishaw has completed the first phase of a £70 million expansion of its manufacturing facility in Miskin, South Wales, as it marks the 15th anniversary of acquiring the site. The development is the largest capital investment project in the company’s history and will ultimately approximately double the facility’s floor space, providing additional capacity for precision metrology, additive manufacturing and position measurement products.
Fifteen years of manufacturing investment in South Wales
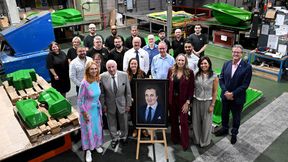
Renishaw acquired the 193-acre former Bosch site west of Cardiff in September 2011. Operations began in May 2012 with a single production shift, following the refurbishment of around 15 percent of the existing 416,000 sq ft (38,675 m²) of building space, primarily comprising two production halls. At the formal opening in October 2012 by the then First Minister of Wales, Carwyn Jones, now Lord Jones, the site employed around 25 people. Today, it employs around 950.
Following completion of Hall 3, usable space has increased to 617,000 sq ft (57,350 m²). This will reach 880,000 sq ft (81,765 m²) once Hall 4 is completed and operational. Around £150 million has been spent to date on acquiring the site, refurbishing existing buildings, developing the new halls and installing manufacturing equipment.
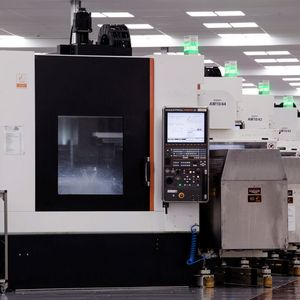
The site currently houses 134 CNC machine tools producing around one million parts per month, three PCB assembly lines, robotic assembly and automated warehousing. Further equipment is on order to support customer requirements. At the original opening, Lord Jones said: “Today is a significant event in the history, not just of this site, but for the whole of South Wales.”
Renishaw manufactures its own products and uses many of them within its machining facilities. Much of its production takes place at its UK sites in Miskin, Stonehouse and Woodchester. The company has also assembled metrology products in Ireland since 1981 and operates a manufacturing facility in Pune, India.
More capacity for metrology and additive manufacturing
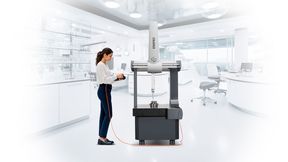
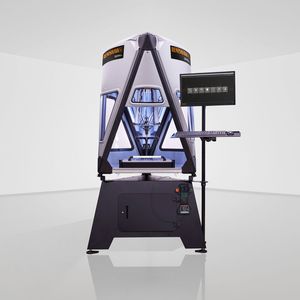
Hall 3 provides 193,000 sq ft of manufacturing space and is now fully operational. It houses production of Renishaw’s metal additive manufacturing systems and Agility coordinate measuring machines (CMMs), alongside a multimillion-pound automated storage and retrieval system. The CMMs inspect complex components for industries including aerospace, automotive, medical technology and renewable energy.
Renishaw reports strong demand for its additive manufacturing systems, particularly from the aerospace and defence sector, as well as growing demand for its high-precision multi-sensor CMMs, including applications in energy, aerospace and defence.
Semiconductor demand brings Hall 4 into use
Hall 4 was constructed as a shell building, with its fit-out dependent on future sales and capacity requirements. Increased demand for position encoders from semiconductor equipment manufacturers, driven by the growing adoption of artificial intelligence, means part of the hall will now be occupied over the coming months. Renishaw is increasing capital expenditure on machine tools, electronics production and automated assembly to support this demand.
The company has already invested tens of millions of pounds in manufacturing equipment for Hall 3 and expects to invest millions more to complete and equip Hall 4. The additional space will allow more flexible production layouts, improved workflows, technology development and pilot production.
Steve Oakes, Director of Position Measurement, said, “Our encoders are used at all stages of the semiconductor production process, from manufacturing silicon wafers to packaging and testing individual devices. The semiconductor sector is highly cyclical, and we are currently seeing a ‘super cycle’, which is driving very high levels of investment across the entire supply chain.”
Designing new and existing buildings for lower emissions
The expansion also supports Renishaw’s target of achieving net-zero greenhouse gas emissions across Scopes 1 and 2 by 2028. Both new halls have been designed to achieve net-zero carbon in operation, while the company’s longer-term ambition is for all buildings at Miskin to operate at net zero. The approach combines reduced building energy demand, electric heating and cooling, and on-site renewable electricity generation.
Date: 08.12.2025
Naturally, we always handle your personal data responsibly. Any personal data we receive from you is processed in accordance with applicable data protection legislation. For detailed information please see our privacy policy.
Consent to the use of data for promotional purposes
I hereby consent to Vogel Communications Group GmbH & Co. KG, Max-Planck-Str. 7-9, 97082 Würzburg including any affiliated companies according to §§ 15 et seq. AktG (hereafter: Vogel Communications Group) using my e-mail address to send editorial newsletters. A list of all affiliated companies can be found here
Newsletter content may include all products and services of any companies mentioned above, including for example specialist journals and books, events and fairs as well as event-related products and services, print and digital media offers and services such as additional (editorial) newsletters, raffles, lead campaigns, market research both online and offline, specialist webportals and e-learning offers. In case my personal telephone number has also been collected, it may be used for offers of aforementioned products, for services of the companies mentioned above, and market research purposes.
Additionally, my consent also includes the processing of my email address and telephone number for data matching for marketing purposes with select advertising partners such as LinkedIn, Google, and Meta. For this, Vogel Communications Group may transmit said data in hashed form to the advertising partners who then use said data to determine whether I am also a member of the mentioned advertising partner portals. Vogel Communications Group uses this feature for the purposes of re-targeting (up-selling, cross-selling, and customer loyalty), generating so-called look-alike audiences for acquisition of new customers, and as basis for exclusion for on-going advertising campaigns. Further information can be found in section “data matching for marketing purposes”.
In case I access protected data on Internet portals of Vogel Communications Group including any affiliated companies according to §§ 15 et seq. AktG, I need to provide further data in order to register for the access to such content. In return for this free access to editorial content, my data may be used in accordance with this consent for the purposes stated here. This does not apply to data matching for marketing purposes.
Right of revocation
I understand that I can revoke my consent at will. My revocation does not change the lawfulness of data processing that was conducted based on my consent leading up to my revocation. One option to declare my revocation is to use the contact form found at https://contact.vogel.de. In case I no longer wish to receive certain newsletters, I have subscribed to, I can also click on the unsubscribe link included at the end of a newsletter. Further information regarding my right of revocation and the implementation of it as well as the consequences of my revocation can be found in the data protection declaration, section editorial newsletter.
For Hall 3, energy modelling indicates that annual base operational energy demand will be met through on-site renewable generation. This relates to building operation, with manufacturing process energy monitored separately. The approach aligns with the UK Green Building Council’s Net Zero Carbon Framework, which addresses energy modelling, renewable generation and verification of operational performance.
Measures were also taken to reduce embodied carbon during construction. Excavated materials were retained and reused on site wherever possible, reducing transport requirements and the need to import or remove large volumes of material.
Existing buildings are being upgraded alongside the expansion. The two original halls acquired from Bosch are due to receive energy-efficient cladding, while legacy heating systems have been replaced with lower-carbon alternatives.
Heat recovery and solar power reduce building energy demand
The new halls incorporate enhanced wall, roof and floor insulation, with thermal performance exceeding current building regulation requirements, according to Renishaw. High-performance glazing further limits heat loss and reduces the energy needed to maintain indoor temperatures.
Electric heat pumps provide heating and cooling, delivering approximately four units of heat or six units of cooling for each unit of electricity consumed. Heat recovery units capture more than 84 percent of the heat from extracted air, while insulated ductwork reduces losses during air distribution.
The development includes 920 m² of roof-mounted photovoltaic panels and 285 m² of wall-mounted panels, with estimated annual electricity generation of around 200 MWh. Renewable electricity tariffs are used for additional supply. On-site generation is intended to reduce reliance on the national grid and exposure to energy price fluctuations.
Monitoring energy use against design predictions
A building management system automatically controls heating, cooling, lighting and ventilation in response to occupancy and weather conditions. More than 150 energy meters in Hall 3 provide real-time consumption data, distinguishing between building services and manufacturing processes to support performance monitoring and identify opportunities for further efficiency improvements.
Building performance will be monitored during the first five years of operation. Energy consumption, renewable generation and system performance will be assessed against design-stage predictions, with any gaps investigated and addressed. The process draws on CIBSE TM54 energy modelling and Soft Landings post-occupancy evaluation.
Investing in employee wellbeing and engineering skills
Alongside manufacturing capacity and energy performance, the development includes investment in employee facilities. A new wellbeing centre provides a restaurant, fitness suite and breakout areas for collaboration, informal meetings and relaxation. Its interior incorporates soft furnishings and a large mural of Pen y Fan, reflecting the surrounding South Wales landscape.
Landscaped outdoor spaces include a central garden with dining areas, lawns and ornamental planting connected to the wellbeing centre. Additional picnic and breakout spaces overlook a wetland basin, while a 2 km perimeter walking route provides opportunities for outdoor activity.
Apprentices and graduate engineers contributed to the expansion project. Project engineering apprentices worked within the design teams for Halls 3 and 4 and the wellbeing centre, helping with layout planning, coordinating with departments, attending site visits and supporting the design of offices and workshops.
The site also houses an education centre supporting the science, technology, engineering and maths curriculum. This forms part of Renishaw’s wider STEM outreach programme for primary and secondary schools in South Wales and the South West of England.
In-house manufacturing supports quality and delivery targets
Jim Long, Director of Group Manufacturing, said, “The strong growth we are currently seeing has highlighted the importance of in-house manufacturing and the control it gives us in meeting our quality, cost and delivery targets. This commitment to manufacturing is exemplified by the investment that we have made in Miskin over the past 15 years and I would like to thank the many people from across our business who have supported the development of this world-class facility.”
He continued, “A key aim of our facilities is to create an attractive and enjoyable working environment that inspires employees while creating a world-class environment that impresses visitors and presents a positive image of manufacturing.”
Long concluded, “The significant ongoing investment by our Board to increase our production capabilities demonstrates a huge vote of confidence in our manufacturing operations and people, at an exciting time for the business.”